Best Stationary Oven Carousel Rotomolding Machine: A Complete Buying Guide
2026-10-06
Finding the right stationary oven carousel rotomolding machine can feel overwhelming—every supplier claims their design is the most efficient, but the real differences show up in daily operation. From arm speed and mold swing to energy consumption and maintenance access, small choices determine whether your line runs smoothly or keeps costing you downtime. This buying guide cuts through the noise and focuses on the features that actually impact your production. We've also looked closely at how manufacturers like Rising Sun address these challenges, so you can compare with confidence.
Matching Carousel Size to Your Actual Production Runs
Most teams pick a carousel based on the largest job they expect to run, but that's usually the wrong starting point. Look at your last six months of production logs and sort runs by actual unit count. If the majority sit between 2,000 and 5,000 pieces with only a few spikes above 10,000, a carousel sized for 15,000 will sit half-empty most days. Those empty pockets add cleanup time and force operators to walk further for no real gain.
A better approach is to treat the carousel as a rhythm setter, not a capacity number. Map out how often you change over between SKUs and how many people actually tend the line during a shift. A smaller carousel that loads and unloads quickly can outproduce a larger one if it cuts fifteen minutes off each changeover and lets one operator stay in reach of the fill nozzles and control panel.
Before finalizing, simulate a typical batch cycle including loading, run time, unloading, and washdown. Do this for two or three carousel sizes using your real order mix. You'll often find that the mid-size option with fewer pockets beats the bigger unit on daily output, simply because it matches the pace of your actual runs instead of a once-a-year peak.
Why Stationary Ovens Punish Weak Insulation Faster Than You Think
Stationary ovens don't cycle like their portable counterparts—they sit at temperature for hours or days, which means any insulation weakness gets a constant workout. Heat doesn't just leak; it finds the path of least resistance and carves it wider over time. A small gap or thin spot in the lining becomes a thermal highway, and the oven's controller responds by driving heating elements harder. That extra duty accelerates element wear and drives up energy consumption far sooner than a simple heat-loss calculation would suggest.
The real punishment comes from the thermal gradient trapped inside the oven wall. Weak insulation lets the outer shell heat unevenly, creating hot spots that stress seals, gaskets, and even the structural frame. Those components expand and contract at different rates, opening microscopic cracks that let moisture in. Once moisture reaches the insulation, its thermal resistance drops sharply—wet mineral wool or fiberglass can lose more than half its insulating value. From there, the degradation curve steepens because the oven now works against both heat loss and the extra thermal mass of absorbed water.
You might expect a linear drop in performance, but field data from repair logs shows otherwise. Ovens with marginal insulation often test fine for the first few weeks, then suddenly show runaway energy use and surface temperatures that climb past safety thresholds. That's the compounding effect: every percentage point of insulation loss forces longer heating cycles, which in turn bakes the remaining insulation and accelerates binder breakdown. By the time an operator notices the outer shell is too hot to touch, the internal damage has already spread well beyond the original weak spot.
Heat Distribution Checks That Reveal Hidden Design Flaws
Thermal cameras and thermocouple matrices often expose what circuit simulations overlook. A board that looks balanced on paper can develop a stubborn hot spot around a connector, a via field, or a power stage when real current flows. Those temperature gradients point to trace necks, missing copper, or plane slots that force current into narrow paths. If one area runs consistently warmer than its neighbors, the layout is telling you something the schematic never will.
Uneven heat across parallel devices is another common giveaway. Two FETs that should share current equally may show a ten or fifteen degree split in steady state. That kind of difference usually means asymmetric trace lengths, poor gate drive routing, or a thermal pad that didn't wet out fully during reflow. The result is one device doing most of the work, aging faster, and eventually failing long before its companion. A quick thermal scan after load testing catches this before it becomes a field return.
Mechanical interfaces also show up clearly in heat distribution checks. A heatsink that makes contact on only two-thirds of its surface area will leave a visible cold stripe on the thermal image. Press-fit connectors, badly soldered pads, and even warped boards all leave their own heat signatures. Because temperature differences appear before outright failure, these checks give you an early warning system for marginal designs that would otherwise pass electrical test.
Mold Arm Loading: The Overlooked Bottleneck in Rotomolding
Walk through most rotomolding plants and the focus lands on oven dwell times, cooling curves, or pulverizing specs. Mold arm loading rarely gets the same attention, yet it can quietly eat more cycle time than any single thermal parameter. When operators hand-fill multiple arms with powder, slight differences in scoop size, pour angle, or compaction create uneven wall thickness part to part. A few extra seconds per arm might seem trivial until you multiply it across a six-arm carousel running hundreds of cycles a month.
Manual loading also introduces variability that no downstream check can fully fix. An operator fatigued by the third hour may under-fill a deep cavity or spill powder around the parting line, leading to thin spots or flash. Because this step depends on feel and repetition rather than a locked recipe, two skilled workers can produce measurably different results on the same mold. The loading station often remains the least automated part of the entire rotomolding line, which is surprising given how directly it affects part weight and scrap rates.
Simple changes can turn this overlooked step into a controlled process. Standardizing the fill sequence for each mold, using vibration-assisted loading funnels, and positioning molds at waist height reduce both time and physical strain. In several shops, measuring fill weight per arm instead of eyeballing volume has cut wall-thickness variation by double digits. No need for a full robotic overhaul, just treat arm loading with the same discipline as oven temperature and the bottleneck starts to disappear.
Comparing Drive Systems Without Getting Lost in Acronyms
If you’ve ever shopped for a car, you’ve likely been hit with a wall of letters: FWD, RWD, AWD, 4WD. They sound technical, but most of them describe something pretty simple—where the engine sends its power. What trips people up is thinking the acronym itself tells the whole story. It doesn’t. A front-wheel-drive car and a rear-wheel-drive car with similar horsepower can feel completely different from behind the wheel, and an all-wheel-drive system isn’t automatically better just because it has more letters. Start by ignoring the badge and asking what actually changes when you accelerate, turn, or hit a slick patch.
Instead of memorizing definitions, think about the physical consequences. With power going only to the front wheels, the car tends to pull itself through corners, which feels stable but can make the steering heavy and numb. Send all that torque to the rear, and the front tires are free to just steer, giving you a lighter, more playful feel—until you add too much throttle mid-corner and the tail steps out. All-wheel drive splits the workload, so launch traction improves and wet roads feel less threatening, but you pay for it with extra weight, worse fuel economy, and sometimes a duller driving character. None of these are flaws on their own; they only become problems if they don’t match how you actually drive.
A smarter comparison ignores the letters altogether and focuses on three things: where you live, how you drive, and what you’re willing to trade. If your commute involves steep, snowy hills, a good AWD system will earn its keep. If you rarely see bad weather and love a nimble car on a back road, rear-wheel drive is worth the learning curve. Front-wheel drive remains the quiet workhorse—cheap to build, easy to live with, and perfectly adequate for most people. Spend less time decoding acronyms and more time test-driving the same car with different drive layouts. The difference hits you within the first sharp corner.
Service Contracts and Spare Parts: What Sellers Don't Volunteer
When you're finalizing a purchase for industrial equipment, the conversation often glides over the less glamorous details. Service contracts and spare parts availability rarely make it into the sales pitch. Yet these are exactly the areas where hidden costs and operational headaches tend to surface months after the handshake. Sellers may mention a warranty period, but they seldom spell out what happens when a critical component fails on a Friday night or how long you'll actually wait for a replacement part that's supposedly 'in stock.'
The real story lives in the fine print. Some vendors require you to buy spare parts exclusively through their network, often at a premium that gets locked in once you sign. Others offer a service contract that sounds comprehensive but excludes the most common failure points or sets response times measured in business days, not hours. Ask direct questions about lead times for specific parts, whether emergency call-outs cost extra, and if there's any penalty for using third-party maintenance. If a seller hesitates or changes the subject, that silence is information too.
Smart buyers treat service commitments as part of the purchase price, not an afterthought. Request a written parts list with current pricing for wear items, confirm whether critical spares are held locally or shipped from overseas, and find out if the contract covers software updates that could otherwise require expensive service visits. A vendor who volunteers this detail before you ask is rare. The ones who resist scrutiny often have the most to hide.
FAQ
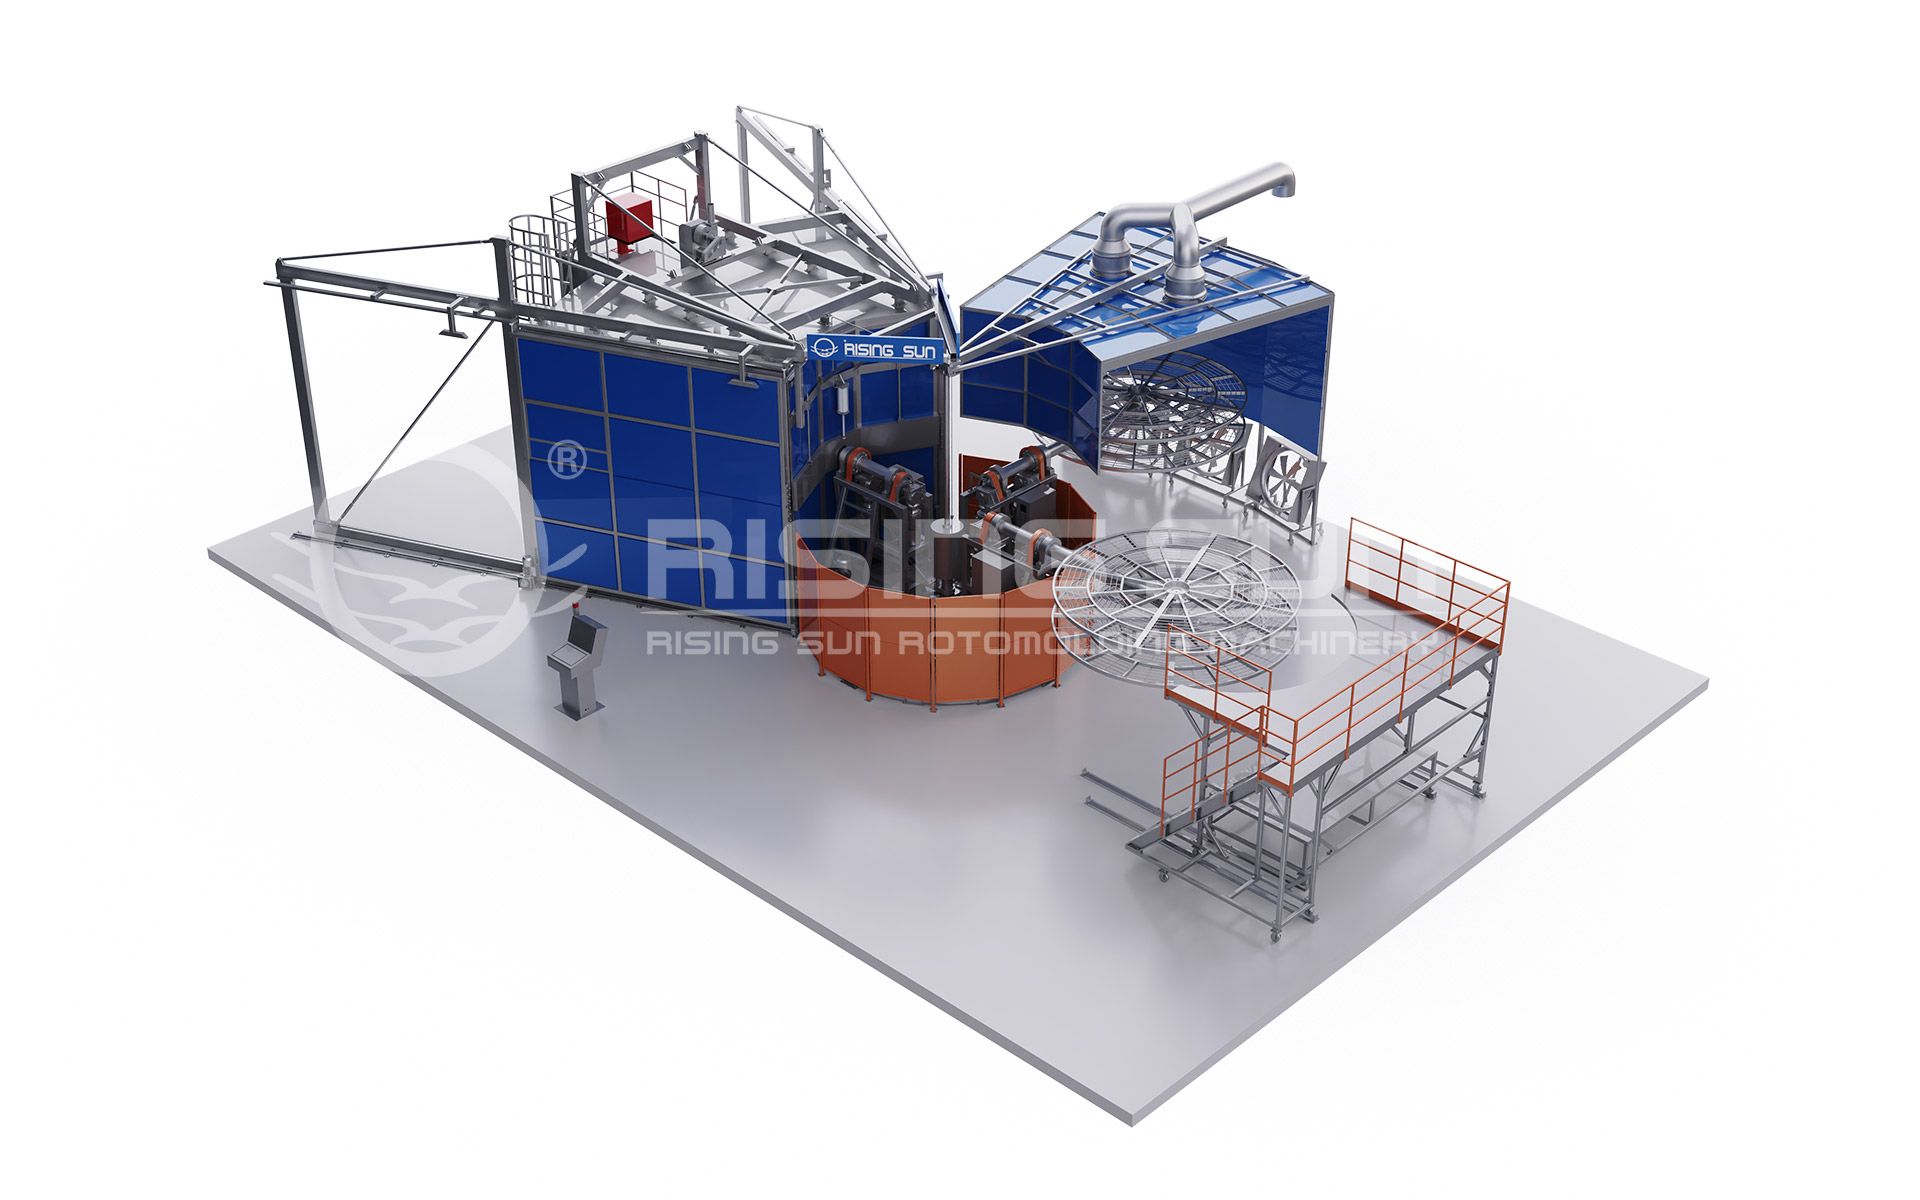
The carousel design keeps the oven in a fixed position while multiple arms rotate molds through heating, cooling, and loading zones. This usually gives you shorter cycle times and more consistent heat exposure than shuttle machines, which move molds back and forth, or rock-and-roll machines that tilt and spin on a single axis. Stationary oven carousel units also tend to use floor space more efficiently because the workstations are arranged around a central pivot.
Look at the number of arms, the diameter of the swing circle, the heating system type, and the cooling method. You also want to confirm the machine's maximum mold weight and diameter per arm, because exceeding those limits shortens bearing life and can warp the frame. Ease of access for mold changes and the control system's programmability matter just as much as raw heating power.
Start with the largest mold you plan to run, including its width, height, and weight. Add clearance for arm swing and part removal, then calculate how many molds you need to produce per hour. A good rule of thumb is to leave at least 15 to 20 percent extra capacity for future mold designs. Undersized ovens force you to slow the cycle or risk uneven wall thickness.
Cast aluminum molds with uniform wall thickness and well-placed vents perform best on a carousel because they heat and cool quickly. Steel molds can work but often need longer cycles. Avoid molds with deep undercuts or very thin cores unless you have auxiliary cooling or a mold-release system, since the fixed arm path can make part ejection more difficult.
Plan for weekly checks of gas lines, burners, temperature sensors, and gearbox oil levels. Monthly, you should inspect the arm bearings, chain or gear drives, and the accuracy of the temperature controllers. Annual maintenance usually includes replacing burner components, cleaning heat exchangers, and recalibrating the PLC. Machines that run near their weight limit all day will need more frequent bearing and seal replacement.
Yes, but you need to clean the oven and mold thoroughly between runs if you use materials with very different melt temperatures or colors. Some processors dedicate certain arms to specific resins to reduce contamination. The control system should let you save and recall recipes for each material's heating profile, rotation speed, and cooling time, which makes changeovers faster and more repeatable.
At minimum, you want interlocks on access doors, emergency stop buttons at each workstation, gas pressure sensors, flame monitoring, and a fume extraction system. Some machines also include automatic shutdown if an arm loses rotation or if the oven exceeds a set temperature. Make sure the control panel gives clear alarms rather than just stopping silently.
Many buyers focus only on price per hour and ignore the cost of mold changeovers or energy consumption. Others underestimate the floor space needed for loading and unloading, or they forget to check whether local gas supply and ventilation can handle the burner output. Choosing a machine with too few arms to stay within budget often creates a bottleneck later, so it's cheaper to size the carousel for your projected growth rather than your current order book.
Conclusion
On paper, many stationary oven carousel rotomolding machines appear similar, but the real differences surface once you match the carousel diameter and number of arms to your actual batch sizes and mold weights. A unit sized for occasional prototyping will struggle in continuous production, while an oversized carousel wastes gas and floor space every cycle. Stationary ovens are particularly unforgiving with weak insulation because the heating chamber stays hot while the cooling and loading stations sit outside it. If the oven walls or door seals leak, you will notice uneven wall thickness and soaring energy bills within weeks, not years. Before committing, run a heat distribution test with wired thermocouples placed at the far corners of the largest mold you plan to rotate. Hot spots near burner inlets and cold zones along the floor reveal whether the oven's airflow and burner placement truly cover the full mold envelope, or whether you will be compensating with longer cycles and extra material.
Mold arm loading often becomes the quiet bottleneck. Check the maximum weight per arm and the distance between stations; if two bulky molds collide during indexing, you lose the flexibility that a carousel is supposed to provide. Drive systems deserve more than a quick glance at acronyms. Ask to see the rotation under full load and confirm the machine maintains smooth bidirectional motion without hesitating at the reversal point, since a jerky drive can create pinholes or uneven powder distribution. Finally, pin down the service contract and spare parts inventory before you sign. Some suppliers quote low upfront prices but stock almost nothing locally, leaving you waiting weeks for a burner control board or a set of high-temperature bearings. Ask for realistic lead times on wear items and whether emergency support includes remote diagnostics or only phone advice. Those answers will tell you more about the true cost of ownership than any glossy specification sheet.
Contact Us
Contact Person: Sharon Zhu
Email: [email protected]
Tel/WhatsApp: 8615712666272
Website: https://www.risingsunroto.com