Optical Comparator Factory Checklist for Quality Assurance Teams
2026-09-23
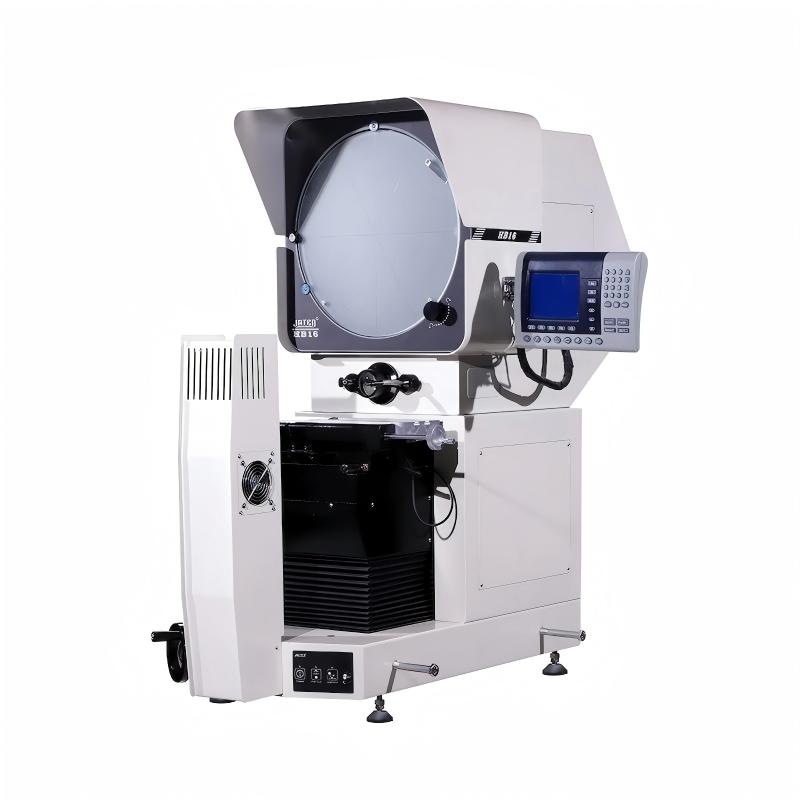
Every quality assurance team knows that an optical comparator is only as reliable as the checks performed before it ever touches a part. Yet factory audits often skim over the basics—lighting alignment, stage travel, lens calibration—until a subtle drift turns into a costly recall. This checklist from JATEN walks you through the often-missed inspection points that keep your comparator trustworthy, so your team can catch dimensional errors before they escape the floor.
Morning Drift Checks That Keep the Comparator Honest
A comparator that hasn't been checked since yesterday afternoon will happily lie to you by mid-morning. Before the first real measurement, I cycle the unit through a zero reference and a known voltage near the upper end of the range we'll use. If the zero reading has moved more than a couple of microvolts from its logged baseline, the rest of the day is already suspect. The drift is rarely dramatic—just enough to nudge a borderline result across a tolerance limit.
Warm-up time matters more than most people admit. Twenty minutes on the bench might stabilize the power supply, but the input stage can keep shifting for another hour if the lab temperature swung overnight. I log readings every ten minutes during that first hour and compare the slope to yesterday's trace. A slow monotonic creep usually means thermal settling; a sudden jump after a half-hour points to a cold solder joint or a tired reference, not normal drift.
The honest check is not just about recording a number—it's about deciding whether the comparator is fit for the work ahead. If the morning drift exceeds the limit we've set for the least significant digit we care about, I don't fight it. I swap in the spare unit, recalibrate the reference chain, and only then start the day's measurements. That small ritual has caught more failing front-end components than any annual calibration ever did.
Aligning Fixtures So Shadows Don't Lie
A misaligned fixture doesn't just cast an odd shadow; it quietly rewrites the shape of whatever sits beneath it. When the beam angle drifts even a few degrees, edges stretch, corners collapse, and a straight table leg can look bowed on the wall. The fix starts before the bulb warms up: check that the housing sits level, the yoke locks evenly, and the lens sits flush against its seat. If the fixture tilts without a reference line, use a plumb bob or a laser level against the mounting plate, not your eye.
Shadow errors compound once multiple fixtures overlap. One fixture aimed slightly inward makes two shadows cross, which reads as a second object or a crack. To keep shadows honest, align each fixture to the same plane first, then walk the space and look at the floor, not the fixture. Shadows should fall parallel unless you deliberately want an angled effect. If they don't, adjust in tiny increments and compare only after the light has stabilised, because a cold lamp shifts its beam.
Lens and Mirror Upkeep Before Every Measurement Run
A quick visual check of all optical surfaces only takes a minute, but skipping it can wreck an entire afternoon of readings. Dust, fingerprints, and even a thin film of lab residue scatter light in ways that quietly inflate your error bars. Get into the habit of catching these issues before the first beam fires, not after the data looks suspicious.
Keep a bulb blower and a fresh pack of lint-free wipes right next to the instrument, not buried in a drawer across the room. For stubborn smudges, breathe lightly on the surface and wipe from center to edge in a single motion—never scrub back and forth. If you spot a scratch or coating delamination, don't try to polish it out; that usually makes things worse. Swap the optic or call someone who handles repairs.
Mirrors and lenses don't need a full deep-clean every day, but they do need the same routine treatment each time you power up. Close the dust caps when the setup sits idle, and keep open containers of solvents or adhesives far away from the optical path. A clean beam path isn't a luxury—it's the difference between a trustworthy measurement and a mystery you'll spend hours chasing.
Spotting Operator Error Faster Than the Manual Allows
Most plants still rely on shift logs and spot checks to catch operator mistakes, which means a wrong valve position can sit unnoticed for hours. Newer monitoring tools pull live data from control systems and flag anomalies the moment a setting drifts outside its normal band. That cuts the gap between error and detection down to seconds, not the next scheduled walkthrough.
The real advantage shows up in complex startups and shutdowns, where procedures run long and fatigue sets in. Instead of asking a tired operator to remember every step against a paper checklist, the system watches sequence timing, pump curves, and interlock states in parallel. A missed confirmation or an out-of-order action triggers an alert while there is still time to correct it safely.
It is not about replacing operators, but backing them with a second set of eyes that never blinks. When a unit trips or a batch runs off-spec, the same pattern-matching logic can replay the last few minutes of operator actions and highlight the exact deviation. That turns a slow, manual investigation into a focused review, often before the shift even ends.
When Logging Deviations, Less Detail Can Hide More Problems
When a process drifts from its expected path, the natural instinct is to jot down a quick note and move on. "Slight temperature rise" or "pressure fluctuated" feels sufficient at the moment, but these terse entries usually strip away the very context that would make them meaningful later. Without recording the exact value, the duration, or what was happening just before the deviation, anyone reviewing the log months later is left guessing whether that blip was a harmless anomaly or an early warning sign.
The deeper problem is that sparse logging actively hides patterns. A series of small deviations, each described with a vague phrase, will never reveal their connections. One "minor voltage drop" on Tuesday and another on Friday might be unrelated, or they might trace back to a failing power supply that only acts up under specific load conditions. But if the log omits the load level, the ambient temperature, or the sequence of operations, the link stays invisible. It's the details—the timestamps, the parameter readings, the order of events—that turn isolated notes into a coherent story.
Of course, writing detailed deviation records takes more effort, and there's always pressure to keep logs short. But every omitted detail is a potential blind spot. The next time you're tempted to summarize a deviation as "nothing major," ask yourself what the person reading this log three years from now will need to know. Chances are, they'll wish you had written down more, not less.
Traceability Audits Without the Last-Minute Scramble
Most audit panic starts with a simple gap: nobody treats traceability records as living documents until the auditor asks for them. A better habit is to fold trace checks into weekly routines. For example, whenever a batch closes, have the line lead verify that raw material lot numbers, equipment logs, and quality checks are linked before the shift ends. This thirty-minute habit spares you from reconstructing a month of spotty entries on a Sunday night.
Another source of last-minute chaos is scattered supplier documentation. Instead of waiting for an audit announcement, ask every supplier to resend current certificates of analysis and origin statements each quarter, and store them in a single folder with a clear naming convention. If you use a digital system, set up automatic reminders for missing attachments. When the auditor arrives, you can pull up any finished product and trace its ingredients back to the receiving dock without chasing emails or digging through filing cabinets.
FAQ
At minimum once per shift, but if you're running tight tolerance parts or the machine gets moved, check it more frequently. A quick verification against a certified glass scale before starting a batch catches drift before it becomes scrap.
Confirm the profile illumination is even across the entire stage and that surface lighting doesn't create glare or shadow on critical edges. Adjust the aperture and filters until the shadow line is crisp—blurry edges will throw off every measurement.
Dust or fingerprints on the lens or mirrors distort the projected image, which directly impacts edge detection and measurement repeatability. Even a small smudge can introduce a few microns of error, so clean optics with approved wipes at the start of each shift.
Keep the unit away from direct sunlight, heavy vibration, and sudden temperature swings. Air currents from open doors or HVAC vents can cause image shimmer, so note whether the comparator sits in a stable zone before trusting the numbers.
Use a certified glass scale or a known master part with documented dimensions. Measure it at multiple points across the stage to catch localized errors. If results deviate beyond your tolerance, stop using the comparator until it's recalibrated.
Log calibration dates, cleaning actions, lamp replacements, and any deviations found during shift checks. This history helps you spot recurring issues—like a lamp dimming over time—before they cause a bad batch to pass inspection.
Confirm each operator knows how to focus correctly, select the right magnification, and interpret edge detection consistently. They should also understand the difference between profile and surface illumination so they don't measure the wrong feature by mistake.
If the stage doesn't travel smoothly or locks slip mid-measurement, your X-Y coordinates become unreliable. A minute of checking travel limits, backlash, and lock tightness each shift prevents subtle shifts that lead to misaligned measurements.
Conclusion
A reliable optical comparator doesn't stay reliable by accident. Each shift should start with a quick drift check against a certified master or a stable reference artifact, because thermal changes and vibration can nudge the optical path enough to turn a borderline part into a false pass. The same morning routine has to include fixture alignment: even a slightly tilted staging surface or worn locating pin will stretch or skew the projected shadow, and once that shadow lies, every measurement downstream inherits the error. Lens and mirror upkeep belongs in the same pre-run pass. Dust, oil haze, or a fingerprint near the projection lens cuts contrast and edge definition long before anyone notices the readings drifting. Wiping surfaces with approved materials and checking for scratches or coating damage takes a minute, but it prevents the kind of subtle blur that operators tend to compensate for by eye, which is exactly the habit a checklist should break.
Operator error rarely announces itself. It hides in rushed fixture loading, inconsistent focus, or repeated use of the wrong magnification setting. A checklist that forces a two-second verification of screen center, edge detection, and part orientation catches these slips before the manual's generic warning would. Logging deviations demands the opposite instinct from what many teams practice: a terse note like "rechecked, OK" hides recurring drift or a damaged mirror that only shows up under certain lighting. Record the actual measured value, the master used, and the corrective action, because those details turn a one-off annoyance into a traceable pattern. Finally, traceability audits should not begin with a frantic search through binders. Keep calibration records, drift-check logs, and fixture inspection dates in a single living document that anyone on the floor can update. That way an auditor's question becomes a ten-minute review instead of a last-minute scramble, and the checklist becomes the reason the comparator earns trust rather than simply passing time.
Contact Us
Contact Person: Volien
Email: [email protected]
Tel/WhatsApp: +86 18029161762
Website: https://www.jatentech.com/